MIM & CIM Technical Insights & Engineering Articles
Industry knowledge, DFM guidelines, material selection whitepapers, and precision powder metallurgy case studies from MIM Supplier.
Precision Ceramic & Metal Molding Innovations
Deep dive into micro-molding tolerances, debinding-sintering processes, and high-purity ceramic solutions for global OEMs.
Design for Manufacturability Best Practices
Practical engineering insights on optimizing part geometries, reducing tooling costs, and achieving 1µm tolerances.
How to Choose Powder Metallurgy Automotive Gears
Table of Contents
- Define the Role and Performance Needs of the Automotive Gear
- Compare Powder Metallurgy Materials and Their Mechanical Properties
- Evaluate Gear Design, Tolerance, and Manufacturing Requirements
- Assess Durability, Noise, Cost, and Production Efficiency
- Select a Supplier and Verify Quality Through Testing and Inspection
- FAQS
- Conclusion
- Related Posts
Choosing Powder Metallurgy Automotive Gears requires more than comparing material prices. Gear teeth may look identical on a drawing, yet their performance can differ significantly. Density gradients, residual porosity, heat treatment, and dimensional change all influence torque capacity, noise, and service life. A gear that survives a bench test may still fail after thousands of cold starts, lubrication changes, or repeated load reversals.
The Metal Powder Industries Federation’s 2023 State of the PM Industry report identifies transportation as a major application area for powder metallurgy components. Its industry data also highlights the continuing importance of automotive production for PM demand. Meanwhile, MarketsandMarkets reports sustained growth in the automotive powder metallurgy market, driven by lightweighting, material efficiency, and manufacturing cost control. These reports support one practical conclusion: selection must connect market expectations with measurable engineering requirements.
Start with the operating profile. Record transmitted torque, rotational speed, duty cycle, temperature, lubricant, and expected mileage. Then compare candidate materials, density levels, surface treatments, and heat-treatment routes. Check tooth accuracy and dimensional stability after sintering. Do not overlook the hub, bore, and mating shaft. Weak interfaces can cancel strong tooth design.
Testing matters.
AGMA design guidance and supplier validation data should support the final choice. Ask for density maps, tensile results, fatigue evidence, and batch traceability. Powder Metallurgy Automotive Gears can deliver quiet, repeatable performance, but only when manufacturing limits match the application. A common mistake is selecting by hardness alone. Real reliability depends on the complete system, and that judgment deserves careful review before production approval.
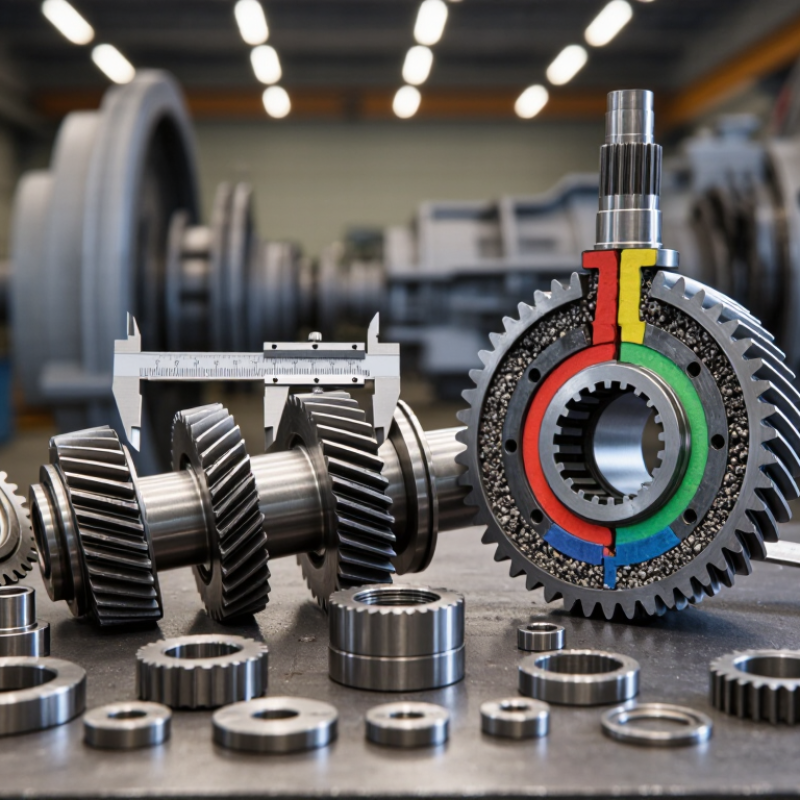
Define the Role and Performance Needs of the Automotive Gear
How to Choose Powder Metallurgy Automotive Gears
Define the gear’s role before selecting its material or manufacturing route. A timing gear needs stable motion and low noise. A transmission gear may face high torque, sudden shocks, and frequent load changes. Record the torque range, rotational speed, duty cycle, temperature, and available space. These details guide decisions about density, tooth strength, hardness, and dimensional tolerance. A gear used near an engine may also need resistance to oil, heat, and vibration. Performance targets must be measurable, not vague. Specify allowable noise, backlash, wear, and service life.
Tips: Build a simple load profile from real driving conditions. Include cold starts, steep climbs, and repeated acceleration. Check mating gear geometry carefully. Small profile errors can create concentrated tooth contact. Prototype testing is valuable, but one test is not enough. Compare results after heat exposure and repeated cycles.
Powder metallurgy can provide consistent shapes and reduced machining, especially for medium-volume production. However, density variation may affect fatigue strength and impact resistance. Do not select a gear only because it meets a drawing dimension. Inspect tooth accuracy, density distribution, surface hardness, and internal defects. I have seen designs pass a static torque test yet show unexpected wear during cycling. That gap deserves attention. Some requirements may also conflict. Higher hardness can improve wear resistance but reduce toughness. Recheck the design when the actual operating data changes.
Compare Powder Metallurgy Materials and Their Mechanical Properties
How to Choose Powder Metallurgy Automotive Gears
Compare Powder Metallurgy Materials and Their Mechanical Properties
Material choice affects gear strength, wear resistance, weight, and cost. Iron-based powder metallurgy grades are common because they offer useful strength and reliable dimensional control. Their performance depends on density, alloy content, sintering, and any later heat treatment. A gear with visible pores may not tolerate repeated impact as well as a denser component. Small details matter.
Copper-infiltrated iron can improve strength and reduce porosity, but it adds weight and process cost. Nickel- or molybdenum-alloyed steels may provide better hardenability and fatigue performance after heat treatment. These gains are not automatic. Tooth-root geometry, lubrication, surface finish, and manufacturing consistency also affect service life. Comparing tensile strength alone can mislead; fatigue and wear data should match the gear’s actual load and operating conditions. I would want those test conditions stated clearly.
Tips: Ask for density, hardness, fatigue, and wear results for the finished gear, not only the raw material. Check whether testing reflects your torque cycles and lubrication. If loads include sharp shocks, validate prototypes under realistic use. A material table helps, but it cannot replace testing. Some uncertainty remains until the gear runs in its intended assembly.
Evaluate Gear Design, Tolerance, and Manufacturing Requirements
Start with the load, speed, and available space. These set the tooth geometry and help determine whether a powder metallurgy gear is suitable. The Metal Powder Industries Federation’s powder metallurgy design guidance emphasizes designing parts around the compaction process. For gears, that means checking whether the tooth form, hub, and web can be pressed and ejected without costly secondary operations. A thick hub beside a thin web may create density variation. It can also complicate tooling. Small details matter.
Set tolerances from the assembly’s actual needs, not from a drawing copied from a machined gear. Specify runout, bore size, and tooth accuracy where each affects noise, mesh, or bearing fit. ISO 1328-1 provides a framework for classifying cylindrical gear accuracy; it does not decide what your application needs. Use test data from prototype gears to connect accuracy limits with measured noise and load performance. Check the bore after sizing, too. It may shift.
Finally, review the production route with the gear supplier: compaction, sintering, sizing, heat treatment, and inspection can each affect dimensions and strength. The MPIF guidance is useful, but real parts still need validation under representative loads. That part is easy to underestimate. Ask for capability data on critical dimensions, not just a nominal tolerance. If testing reveals variation, revisit the design before tightening every limit. Tighter is not automatically better.
Assess Durability, Noise, Cost, and Production Efficiency
Durability starts with load, density, and tooth-root geometry. Specify torque cycles, lubrication, and shock loads before comparing materials. MPIF’s Materials Standards for PM Structural Parts provides recognized material and testing references; use its data alongside supplier test results, not as a substitute. Ask for fatigue-test conditions, density maps, and failure photos. A shiny surface proves little. For gear accuracy, ISO 1328-1 gives a common classification framework, while ISO 6336 helps assess load capacity. Neither standard alone predicts performance in your exact gearbox.
Noise depends on more than tooth accuracy. Check backlash, runout, surface finish, and housing resonance on assembled units. Record sound levels at defined speed, torque, temperature, and microphone position; otherwise, comparisons can mislead. Powder metallurgy can combine several features in one part and support high-volume production, but tooling costs and secondary sizing or machining may change the economics. Compare total cost per accepted gear, including scrap, inspection, and finishing—not just the quoted part price. Small batches may tell a different story.
Select a Supplier and Verify Quality Through Testing and Inspection
Choosing a powder metallurgy gear supplier starts with process transparency, not a low quote. Ask how the supplier controls powder composition, compaction pressure, sintering temperature, and furnace atmosphere. These details affect density, tooth strength, and dimensional consistency. Request sample inspection reports and confirm they match the exact gear design and production route. A supplier should explain how it handles tool wear and process changes between production runs. A polished brochure is not evidence. I would also ask to review a recent corrective-action record; it can reveal how openly the team addresses variation.
Agree on acceptance criteria before ordering production parts. Check gear dimensions, tooth profile, runout, and surface condition against the drawing. Measure density at specified locations, since an average can hide weak areas. Hardness testing and metallographic review can help verify the sintered structure, while tooth-bending or fatigue tests may suit demanding applications. Use a defined sampling plan, and retain traceable results by lot. Test parts under representative loads when possible. One caveat: inspection cannot compensate for unclear specifications. Even experienced teams sometimes discover that a test fixture masks a real contact pattern issue, so correlate bench results with gear-mesh checks in the intended assembly.
How to Choose Powder Metallurgy Automotive Gears - Select a Supplier and Verify Quality Through Testing and Inspection
| Evaluation Dimension | Recommended Technical Target | How to Verify | Typical Acceptance Guidance | Priority |
|---|---|---|---|---|
| Material definition | Documented iron-based powder composition, alloying elements, lubricant system, and heat-treatment condition. | Review the material specification, powder certificate, lot traceability, and change-control procedure. | Every production lot should be traceable to raw material, pressing, sintering, sizing, and finishing records. | Critical |
| Density and porosity | Use a density range appropriate to the gear design; many structural iron-based PM gears are commonly specified around 6.8–7.4 g/cm³, subject to material and load requirements. | Measure density by an approved immersion or dimensional method and examine pore distribution by metallography. | Require uniform density in high-load regions and prohibit interconnected defects that could reduce tooth-root strength. | Critical |
| Dimensional capability | Stable control of tooth thickness, outside diameter, bore, face width, keyway, and datum features. | Use calibrated coordinate measuring machines, functional gauges, optical measurement, and control charts. | Dimensions must meet the approved drawing tolerances at room temperature, with measurement uncertainty documented. | Critical |
| Gear accuracy | Define the required accuracy grade for profile deviation, helix deviation, pitch variation, and radial runout. | Inspect with a calibrated gear-measuring machine in accordance with the applicable gear accuracy standard, such as ISO 1328. | The measured grade should satisfy the drawing or application requirement across the complete tooth circumference. | Critical |
| Tooth surface condition | Controlled tooth roughness, absence of loose particles, cracks, laps, burrs, and abnormal surface tearing. | Perform visual inspection, tactile checks, surface roughness measurement, and magnetic-particle or dye-penetrant testing where applicable. | No cracks or loose sintered particles are permitted in the tooth flank, root, bore, or other fatigue-sensitive areas. | Critical |
| Heat-treatment consistency | Uniform case depth, hardness profile, core hardness, and microstructure when carburizing, carbonitriding, or other hardening is specified. | Check surface and core hardness, hardness gradients, effective case depth, and etched cross-sections by metallographic examination. | Acceptance limits must be defined by the gear design; reject soft spots, excessive retained austenite, decarburization, or abnormal grain structure. | Critical |
| Hardness verification | Specify hardness scales and locations separately for tooth flank, tooth root, core, and bore when applicable. | Use calibrated Rockwell, Vickers, or microhardness equipment with a defined sampling plan. | Results must remain within the drawing range and show no unexplained lot-to-lot drift. | High |
| Tooth-root strength | Adequate bending fatigue strength for the calculated torque, speed, shock load, and service life. | Conduct static proof, bending fatigue, or component endurance testing using representative production parts. | Define load, speed, lubrication, temperature, cycle count, and failure criteria before testing. | Critical |
| Pitting and wear resistance | Tooth flank material and surface finish must withstand contact stress, lubrication conditions, and expected duty cycles. | Perform rolling-contact or gear endurance testing and inspect for pitting, scuffing, plastic flow, and abnormal wear. | No progressive damage beyond the agreed engineering limit after the specified test duration. | Critical |
| Runout and balance | Controlled radial runout, face runout, bore concentricity, and mass distribution. | Measure on precision fixtures using dial indicators, roundness equipment, or coordinate measurement; perform dynamic balancing where required. | Limits should be linked to operating speed, bearing arrangement, noise targets, and assembly tolerances. | High |
| Noise and vibration performance | Stable transmission error, low gear whine, and acceptable vibration under the specified operating load and speed. | Use a dynamometer or gear test rig with calibrated microphones, accelerometers, and order-tracking analysis. | Set measurable noise and vibration limits for defined speed, torque, temperature, lubricant, and assembly conditions. | High |
| Supplier process capability | Stable pressing, sintering, sizing, machining, heat treatment, cleaning, and inspection processes. | Review process flow, PFMEA, control plan, gauge calibration, statistical process control, and nonconformance records. | Critical characteristics should have defined controls, reaction plans, and demonstrated capability using production-equivalent equipment. | Critical |
| Lot acceptance and sampling | A documented sampling plan covering appearance, dimensions, density, hardness, gear accuracy, and functional testing. | Audit inspection records and compare sample frequency with product risk and customer requirements. | Use 100% inspection for safety-critical or easily automated characteristics when justified; use statistical sampling for stable attributes. | High |
| Validation documentation | Complete first-article, material, dimensional, metallurgical, durability, and change-validation reports. | Check test reports for part numbers, revision levels, equipment identification, calibration status, raw data, and approval signatures. | Reports must be reproducible, traceable to production lots, and retained for the agreed product life. | High |
| Change management | Formal approval for changes to powder, tooling, press parameters, sintering profile, heat treatment, machining, or inspection methods. | Review the supplier change-notification process and evidence of requalification after significant changes. | No production or material change should be implemented without documented risk assessment and customer approval when required. | Critical |
Note: Final acceptance limits should be established from the approved gear drawing, vehicle duty cycle, lubrication conditions, applicable standards, and validated test results.
FAQS
Define the gear’s role, torque range, speed, duty cycle, temperature, and available space. A timing gear needs stable motion and low noise. A transmission gear may face shocks and changing loads. Performance targets should include noise, backlash, wear, and service life.
Build a load profile from cold starts, steep climbs, and repeated acceleration. Include temperature changes and sudden torque increases. Check the mating gear geometry carefully. Small profile errors can concentrate contact on one tooth area.
Powder metallurgy can produce consistent shapes with less machining. It may suit medium-volume and high-volume production. Several features can sometimes be formed in one part. Tooling and finishing costs still require careful review.
Density variation may reduce fatigue strength and impact resistance. Average density can hide weak internal areas. Inspect density at defined locations. A gear may pass static torque testing yet wear during repeated cycling.
Test torque cycles, lubrication conditions, shock loads, and operating temperatures. Review tooth-root geometry and surface hardness. Request fatigue-test conditions, density maps, and failure images. One test can mislead. Repeated testing is wiser.
Measure noise at fixed speed, torque, temperature, and microphone position. Check backlash, runout, surface finish, and housing resonance. Test gears inside the intended housing when possible. A quiet bench result may change after assembly.
Compare the total cost per accepted gear. Include tooling, scrap, inspection, secondary sizing, machining, and finishing. Do not rely only on the quoted part price. Small batches may produce different economics. The cheapest route is not always practical.
Ask how powder composition, compaction pressure, sintering temperature, and furnace atmosphere are controlled. Request inspection reports for the exact gear design. Review tool-wear controls and production-change procedures. A polished brochure proves little. Recent corrective-action records may reveal process honesty.
Check dimensions, tooth profile, runout, surface condition, density, hardness, and internal structure. Use a defined sampling plan with traceable lot records. Demand representative tooth-bending or fatigue testing for demanding applications. Correlate bench results with gear-mesh checks. Inspection cannot repair unclear specifications.
Conclusion
Choosing Powder Metallurgy Automotive Gears begins with clearly defining the gear’s function, load conditions, speed, operating temperature, and expected service life. These requirements guide the selection of suitable powder metallurgy materials and help determine the necessary strength, hardness, wear resistance, and dimensional stability. Designers should also evaluate tooth geometry, tolerances, surface finish, noise requirements, and compatibility with the intended transmission system to ensure reliable performance.
A complete evaluation should balance durability, operating noise, production cost, and manufacturing efficiency. Powder metallurgy can support high-volume production and consistent near-net-shape components, but the process must be matched to the gear’s design and performance demands. When selecting a supplier, manufacturers should review process capability, material control, dimensional consistency, and quality management practices. Testing and inspection, including density checks, dimensional measurement, hardness evaluation, and functional performance testing, are essential for confirming that the finished gears meet technical specifications and provide dependable service.
Blog Tags: